### 1. The Purchase Price Illusion in CNC Capital Investments
In industrial manufacturing, the initial purchase invoice represents only **20% to 30% of a machine tool's total lifecycle cost over a 10-year operating horizon**.
The remaining 70% is consumed by: - Scrap rates caused by thermal drift and loss of positioning repeatability. - Unplanned downtime and spindle rebuild frequency. - Operator cycle inefficiency and maintenance parts sourcing delays.
---
### 2. Where Precision Degrades: The Metallurgical Reality
Low-cost machine tools frequently bypass **natural or vibrational stress-relieving cycles** on their cast iron beds. Within 12 to 24 months of heavy shop floor thermal cycling, latent stresses in the casting relieve themselves, resulting in: 1. Bed twist (leads to tapers in long shaft turning). 2. Spindle headstock drop (causes out-of-squareness in vertical milling). 3. Ball screw elongation and backlash increase.
At **DRC Machinery**, all castings undergo **Meehanite foundry standards**, followed by secondary heat aging and outdoor weather conditioning to guarantee that structural stability is locked in prior to precision slideway grinding.
---
### 3. Laser Interferometer Calibration: The Sub-Micron Benchmark
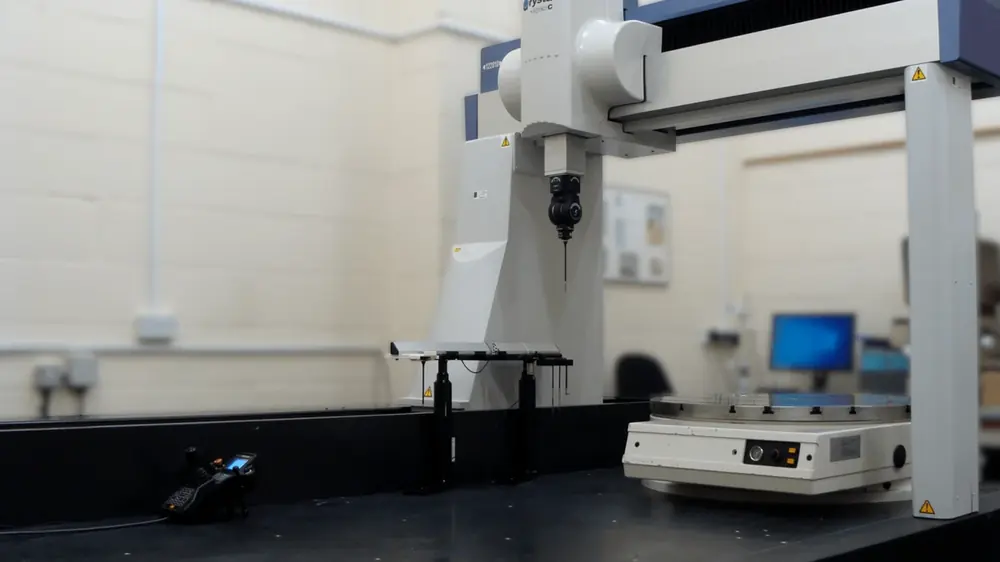
Every DRC machine undergoes 100% full-stroke pitch error compensation utilizing **Renishaw dual-beam laser interferometers**: - Backlash compensation down to **0.001 mm**. - Multi-point positional verification across the full X, Y, and Z travel. - Circularity and dynamic servo tuning verified by **Renishaw QC20-W Ballbar testing**.
---
### 4. 10-Year TCO Comparison Table
| Operational Factor | Generic Low-Tier CNC | DRC Machinery Machine Tools | | :--- | :--- | :--- | | **Bed Casting Quality** | Unaged gray iron | Aged Meehanite dense-grain alloy | | **Laser Calibration** | Sampling only | 100% full-axis Renishaw calibration | | **Guideway Hardness** | HRC 45 - 48 | Induction Hardened HRC 52 - 55 | | **Yearly Scrap Rate** | 2.5% - 4.0% | < 0.4% consistent tolerance | | **Expected Spindle Life** | 8,000 - 12,000 hours | 25,000+ hours with oil cooling | | **Total 10-Year Net Cost** | **$215,000+** | **$128,000** |
*Contact our sales engineering team at xiuc32860@gmail.com to calculate your custom payback period.*
Application Engineering Advisory
Have specific machining tolerances or difficult alloy workpieces?
Send your engineering drawings or material specifications directly to our senior CNC application engineering desk. We provide comprehensive cycle time calculations, tool path suggestions, and recommended machine configurations within 24 hours.
Related Engineering Articles
Engineering Guide
Slant Bed vs Flat Bed CNC Lathe: The Complete Engineering & Buyer Guide
Understand how structural geometry, thermal expansion vectors, chip evacuation dynamics, and tooling ergonomics dictate whether your plant needs a 45° slant bed (TCK series) or a universal flat bed (CK series).
Machining Centers
Selecting the Right Vertical Machining Center: BT40 vs BT50 and Linear vs Box Ways
A deep dive into spindle taper geometry, torque-power curves, and axis guideway rigidity to maximize productivity in aluminum high-speed milling versus heavy mold steel roughing.